Vacuum technology for beer bottling
Many beverages are prone to oxidation processes once they are served in a glass. Some beers can deteriorate within minutes after being poured. That is why breweries take the effort to fill bottles using vacuum technology, as lowering the oxygen content in the product can significantly increase the shelf life time.
What sounds straightforward from a brewer’s point of view, creates a big headache for those involved in vacuum technology.
In principle, removing the air from a glass bottle is a very simple task, which was successfully achieved more than a hundred years ago. Today’s modern bottling machines, however, are filling 60,000 bottles per hour or even more. Emptying a bottle, purging with CO2 and filling happens within seconds. Some spillover is basically unavoidable, not only in the case of a malfunction. Thus, a significant amount of liquid will be dragged to the vacuum system.
Vacuum pumps are made to compress gases from low to atmospheric pressure. Liquids, however, are basically incompressible. (For example, one can easily push the piston of a bicycle tyre inflator even though the valve is blocked; however, this is impossible if the pump is filled with water1).
Even worse, the liquid, basically water, which might come to the vacuum system can undergo a phase transition (evaporation) due to temperature rise. Vacuum pumps can easily generate internal temperatures of more than hundred degrees — enough to evaporate all liquid water. Only 18 g of liquid water, which takes a volume of roughly 18 mL, will take about 24 L of volume if evaporated at room temperature — a factor of 1333. Apart from possible generation of overpressures, evaporation inside of pumps can severely disturb the thermal management; in particular, so-called dry pumps which operate without any lubricant in the suction volume.
Nonetheless, the biggest threat for vacuum systems might come from the various ingredients of beer, which can form deposits. Sugars and starch, originating from malt and transported by droplets, can form hard layers, for example, by caramelising. No matter which pump technology is chosen, early pump failures are possible — even likely.
The best way to protect a vacuum pump system is by separating the liquid content from the gaseous one. There are numerous solutions at hand to separate liquids, mostly in the form of droplets, from gas streams. Cyclones use the high inertia of droplets in concentric gas streams. The centrifugal force pushes the liquid particles with higher density than the gas to the wall of the cylinder, whereas the gas molecules can escape through the centred exit of the vessel. Filters with cartridges tailored for specific applications can remove basically all relevant particles coming from the process but they might reduce the suction speed, in particular, if they are blocked.
Unfortunately, things are even more complicated in case of beer bottling. The reason for this is foam.
Importance of a good foam
For some beer drinkers, the foam or head of a good beer is even more important than the delicious liquid below it. The foam is anything but a by-product of fermentation and the release of carbon dioxide — it is a definite design element.
The beer coming to the vacuum system is basically forced to foam. Apart from foam generated by turbulent flow of the liquid, which causes generation of gas inclusions, there is the steady release of CO2 from the liquid.
However, the release of carbon dioxide itself is not sufficient to create foam. Numerous ingredients of beer act as surfactants, which enable the formation of stable bubbles on top of the liquid.
The solubility of a gas in a liquid is described by Henry’s law, which basically states that the ratio of gas in the gas phase on top of a liquid to the gas dissolved in the liquid is constant — the Henry constant.
The solubility of CO2 in water is extraordinarily high due to the formation of carbonic acid H2CO3 and its ionic dissociation products (bicarbonate HCO3- and carbonate CO32-).
Opening a beer bottle means lowering the inner pressure, typically less than 6 bar (limited by the pressure relief of the crown cap), to atmospheric pressure. Beer coming to the vacuum system is exposed to even 10 times lower pressure, which inevitably causes release of CO2.
Even though the beer in an opened bottle is a highly supersaturated liquid, the bubble formation hardly occurs in the liquid itself. Whoever has watched the sparkling in a glass carefully knows that bubbles appear at the glass surface. Nucleation spots are typically little imperfections with increased roughness on the microscopic scale. While perfectly flat surfaces can be easily covered with the liquid, microscopic indentations cannot be filled due to the surface tension. This is where gas released from the beer can accumulate. In order to further grow and to form a bubble a certain radius needs to be overcome. The reason for this is the Laplace pressure2 which determines the inner pressure of a bubble can be so high that the gas dissolves again in the liquid easier than gas diffuses into the bubble. Small bubbles will therefore shrink and vanish especially if fully surrounded by the liquid (homogeneous nucleation). Conditions at rough surfaces are more beneficial for the bubble formation (heterogenous nucleation). Small crevices can shelter the gas from high Laplace pressures and finally enough gas can accumulate to develop gas bubbles big enough. As the Laplace pressure decreases with the radius, diffusion of gas into the bubble becomes energetically more favourable and the bubble can grow further. At a certain size the buoyancy will force the detachment of the bubble and it will rise to the surface.
One can observe this behaviour in basically every glass but at best in glasses with so called moussier points (also called effervescence point). These are spots with deliberately increased roughness, which trigger intense bubble formation.
On its way up, the bubble will grow a bit more because the pressure caused by the weight of the liquid above it will decrease. One can roughly calculate one mbar pressure reduction per cm. Even in tall glasses the overall pressure reduction, therefore the bubble growth, is minor in view of the atmospheric pressure (ca. 1000 mbar) which remains unaffected and needs to be added.
Reaching the beverage’s surface means life’s end for most bubbles. Mineral water and sparkling wine are well-known examples. For beer in turn bubbles can survive at the surface, thanks to ingredients acting as surfactants.
Proteins (LTP1, Z, ...) coming mainly from wheat malt, iso-alpha acids from hops and polysaccharides are only some of the surfactants that favour foam formation and stabilisation (Bamforth 2004). Counteracting substances are also present in beer suppressing foam formation. Lipids, free fatty acids and last but not least, ethanol are negative for foam formation.
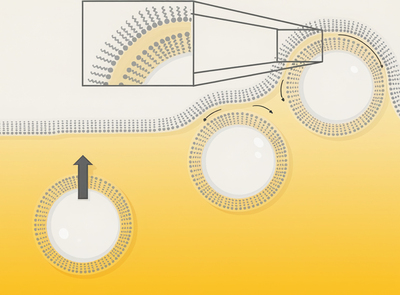
The complex interaction of these ingredients results in a surface tension of beer that is lower than that of water. While water has a surface tension of about 73 mN/m, typical beers cover a range from 40–50 mN/m. Pure water, of course, is not able to foam. However, it is important to note that water-based soap solutions that are used to make soap bubbles typically have even lower surface tension values, which helps to stabilise the very thin films down to some nanometres. These small film thicknesses are the reason for soap bubbles being so colourful. Interference effects of reflected light at inner and outer surface can cause different wavelengths of visible light (ca. 400–800 nm) to extinguish.
Fortunately, such thin wall thicknesses of bubbles are hardly realised in beer foams. In addition, multiple scattering of light in beer foams ensures the typical, nice white appearance.
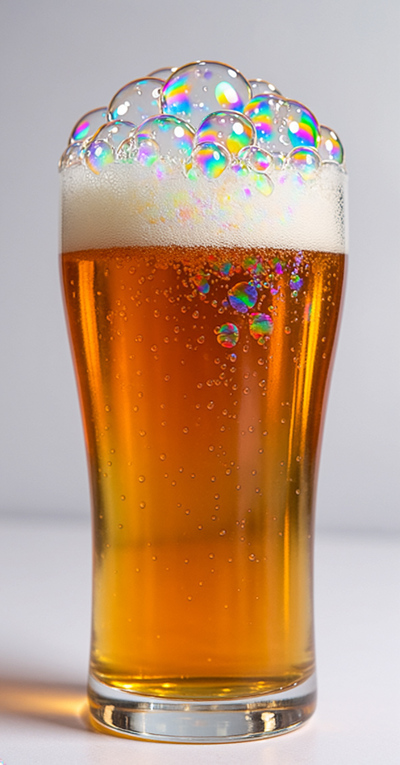
One might hope that beer foam under vacuum simple bursts. Simply by applying the ideal gas law (pV=nkbT=>p1V1=p2V2 if T=const.), one can see that a foam bubble at 0.1 bar takes 10 times the volume than at 1 bar. Certainly, this reduces the thickness of the film of the bubbles. The new thickness can be approximated by : x' = xa–2/3, with a being the increase in volume a = V2/V1 and x' and x being the thickness after and before volume increase, respectively3. The initial thickness of the bubble’s skin only reduces to (V2/V1)(-2/3) = 0.21, roughly one-fifth of the initial thickness.
However, hoping foam will simply burst under vacuum because the volume increases is not successful. From touching the liquid’s surface due to buoyancy to final rupture of the foam’s bubbles, the thickness of the wall between two bubbles can change by orders of magnitude.
This is nicely demonstrated in Leybold’s beer glass experiment (Leybold 2017). It shows the growth of bubbles due to lowering the ambient pressure. At the end, huge bubble sizes gush out of the glass. One can also observe that the bubble shape is everything but round. The formation of Plateau4 borders is well known for foams with thin film boarders. In general, due to the surface tension, a sphere-like shape of a bubble is energetically favourable. For two bubbles next to each other with hardly any liquid between them, this condition cannot be fulfilled for both bubbles at a time. The result is a flat border showing no curvature. The foam structure with several of such bubbles with hardly any liquid between them (‘dry foams’) follows the Plateau’s laws: three films meet at a Plateau border at an angle of 120° and at a vertex four Plateau borders form a tetrahedron with an angle of 109.49° between them.
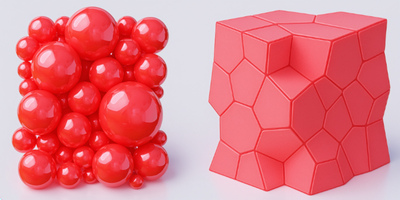
For beer foam, however, this behaviour is hardly observable. The reason is, that it typically stays wet throughout the life-time. There are different deterioration mechanisms for foams; not all of them are equally important for beer.
Drainage describes the — gravity-driven — flow of liquid from the foam back to the liquid phase. It is the major mechanism thinning the film between two bubbles. Stabilising mechanisms like the Marangoni or Gibs-Marangoni effect (the liquid moves to regions with high surface tension due to a gradient of the surface tension) counteracts and prevents early rupture.
In fact, foam deterioration-mechanisms like bubble rupture or coalescence are hardly observed in foams of beer — unlike in other types of foam. The head of a beer can be remarkably stable depending on the type of beer.
Ostwald ripening, sometimes referred to as disproportionation, describes the favoured growth of bigger bubbles at the expense of smaller bubbles. Here again the higher Laplace pressure of smaller bubbles drives the diffusion of gas into bigger bubbles.
At the top layer of foam bubbles CO2 will quickly diffuse to ambient due to the difference in partial pressure — an important effect for foam aging. For some beers this effect is effectively mitigated by adding nitrogen. The low solubility of N2 in aqueous solutions and the high amount of nitrogen in air hampers the gas exchange.
From a vacuum technology point of view, foam is a very challenging opponent. Cyclons can hardly separate small foam fragments because the effective density (and therefore the inertia) can be close to the one of the gas.5 Filters, in turn, will always lower the suction speed of the vacuum pump system. Once clogged the reduction in performance will be even worse. Wet foams can even penetrate filters and the liquid downstream can create new foam also triggered by the pressure drop across the filter element.
Clearly the best method to handle foam in a vacuum system is to avoid foam. There are numerous chemical ways to do this. Unfortunately, food applications are highly sensitive to any kind of chemicals that might contaminate their product. No brewery will accept the risk of this, even though it might only occur during rare malfunctions.
There are also other ways of defoaming. Ultrasonic defoaming, for example, relies on resonance effects on foam bubbles with diameters that are in the range of the acoustic wavelength. Mechanical removal of foam is rather trivial, of course. Both methods are not easy to apply under vacuum conditions.
An interesting approach for passive foam control is surface treatment. Recent studies of superamphiphobic surfaces show remarkable results. Nanoparticle-based surface coatings establish an air gap where gas bubbles can burst and release the gas before reaching the liquid’s surface and contributing to foam growth (Wong, Naga und Hauer 2021).
Technically, probably the most resistant pumping solution are water ring pumps, but these come along with high water consumption and clearly less energy efficiency, means more energy consumption than modern pumping solutions. The constant rotating liquid ring intrinsically causes higher fractional losses than rotating mechanisms based on oil lubrication or even without any sealing agent — so called “dry” pumps. Water ring pumps can become more efficient if there is a considerable condensation effect inside of the pump but as the main constituents of the gas mixture in beer bottling are air and carbon dioxide, basically no condensation will take place. The difference in efficiency (= pumping speed/power) can easily reach 20–30%, which means 40 (m3/h)/kW instead of 50 (m3/h)/kW. Pressures considerably lower than 100 mbar, which might be required in beer bottle filling, become even more challenging for LRPs. At 10 mbar modern dry screw pumps can reach efficiencies of more than 90 (m2/h)/kW — a pressure not reachable for LRPs.
Oil-sealed vacuum pumps can be found in beer bottling even though this technology inevitably comes with the risk of back contamination of the product (for example in case of accidentally venting the system through the pump). Therefore, so-called “food-grade” oils can be used as lubricants for the pumps. However, a food scandal will be hardly mitigated if customers learn that it was food-grade oil in their beer. Apart from this, every lubricant will be sensitive to even small amounts of carry-overs from the filling process. Moreover, flushing out or dissolving process material is impossible as the flushing agent inevitably will mix with the lubricant.
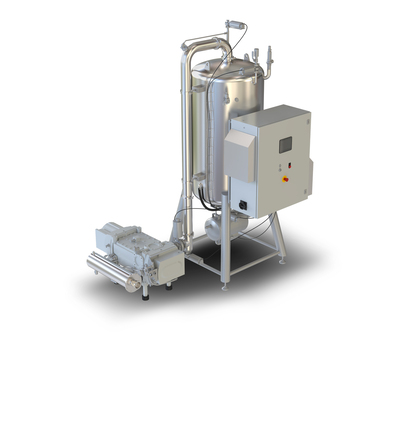
Dry pump technology, not using any lubricant in the suction chamber, can be flushed and might be the best pumping technology as long as carry-over from the filling process cannot be fully avoided.
Still today, foam is a challenging opponent for vacuum systems.
1. The company doesn’t recommend filling neither inflators nor tyres with water unless for experimental studies.
2. 𝑝𝐿𝑎𝑝𝑙𝑎𝑐𝑒= 2𝛾/𝑟 for bubbles surrounded by the liquid and 𝑝𝐿𝑎𝑝𝑙𝑎𝑐𝑒= 4𝛾/𝑟 for free bubbles, 𝛾 being the surface tension.
3. The approximation assumes 𝑥≪𝑅 which is normally fulfilled. The exact calculation yields: 𝑥′=−𝑅𝑎13+[(𝑅3𝑎+3𝑅2𝑥+3𝑅𝑥2+𝑥3)]13 with 𝑅 being the initial radius.
4. Joseph Antoine Ferdinand Plateau, Belgian physicist, 1801–1883.
5. For bubbles with a radius of 1 mm and a film thickness of 100 nm the film’s weight only contributes about 30% to the overall weight.
The role of heat exchangers in alcohol-free brewing
Alcohol-free drinks are produced in a similar way to conventional beers and ciders so the...
In-shell nut inspection system finds hidden product defects in pecans
Payne's Pecans uses a bulk X-ray system to identify hidden defects, increase throughput and...
Dual conveying systems automate chocolate cream production
In order to produce its new 'Chocolate Dodger' biscuit, Burton's Biscuit installed a...