Contamination detection solutions for the food manufacturing industry
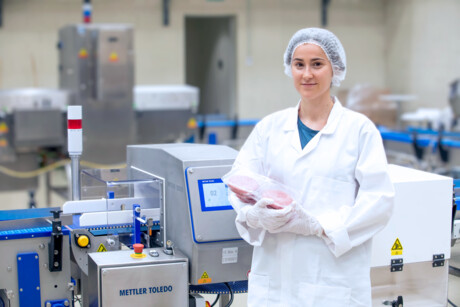
In the highly regulated food manufacturing industry, ensuring product safety and quality is essential to protecting consumers, maintaining brand reputation, and meeting regulatory requirements. Even a single contamination incident can result in product recalls, financial losses, regulatory penalties, and long-term damage to consumer trust.
To help manufacturers address these challenges, METTLER TOLEDO provides reliable and cost-effective contamination detection solutions designed to meet a wide range of inspection needs. These advanced systems help safeguard products while improving operational efficiency and quality control.
One of the biggest challenges food manufacturers face is the risk of foreign object contamination. Materials such as metal fragments, glass, stone, plastic, or bone can accidentally enter products at various stages of production. If undetected, these contaminants can pose serious health risks to consumers and lead to costly recalls and reputational damage.
Maintaining consistent product quality is equally important. Issues such as incorrect fill levels, damaged packaging, faulty seals, or missing components can negatively affect customer satisfaction, product shelf life, and compliance with industry standards. Manufacturers therefore need inspection systems that support both contamination detection and quality assurance.
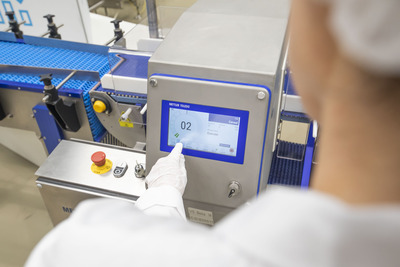
METTLER TOLEDO’s X-Ray inspection technology goes beyond traditional contamination detection by identifying a wide range of foreign materials regardless of packaging type. The systems can reliably detect metal, glass, stone, dense plastic, and bone, helping ensure only safe products reach consumers.
In addition to contamination detection, the systems perform critical quality checks, including:
- Verifying product fill levels
- Inspecting seal integrity
- Detecting missing or damaged components
- Identifying packaging inconsistencies
This multifunctional capability makes X-Ray inspection a valuable tool for maintaining both food safety and product quality.
Key Benefits for Food Manufacturers
Enhanced Food Safety
METTLER TOLEDO X-Ray systems help protect consumers by detecting and rejecting contaminated products before they leave the production line. By preventing foreign materials from reaching the market, manufacturers can reduce risk and strengthen consumer confidence in their brand.
Regulatory Compliance
The systems support compliance with food safety programs and regulations, including HACCP and FSMA. Consistent monitoring, inspection, and documentation help manufacturers remain audit-ready and meet evolving industry requirements.
Reduced Waste and Recalls
Early detection of contaminants and defects minimises the risk of costly recalls and reduces product waste. Reliable inspection helps manufacturers identify issues before products enter distribution, resulting in significant cost savings and improved operational performance.
Improved Operational Efficiency
Designed for high-speed production environments, METTLER TOLEDO systems integrate seamlessly into existing lines without compromising throughput. Automated inspection and rejection processes reduce manual intervention, improve productivity, and support continuous production.
Versatility Across Applications
The systems can inspect a wide variety of food products and packaging formats, including bakery, dairy, meat, seafood, and confectionery applications. This flexibility allows manufacturers to standardise inspection technology across multiple product lines.
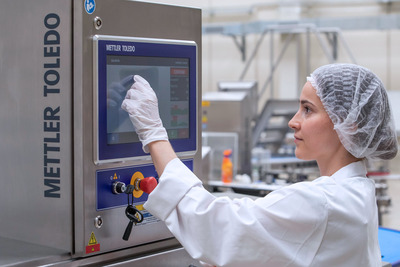
Beyond performance, METTLER TOLEDO systems are designed with hygiene in mind. Stainless steel construction, smooth surfaces, and accessible cleaning areas help prevent contamination build-up, reduce cleaning time, and support compliance with strict sanitation standards.
With decades of industry experience, METTLER TOLEDO delivers solutions that combine precision, reliability, and ease of use. Intuitive interfaces and customisable settings enable manufacturers to tailor inspections to their specific production requirements, while comprehensive training, maintenance, and technical support ensure long-term success.
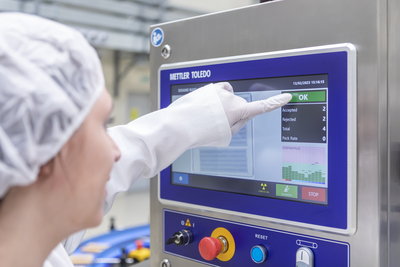
The systems also support data-driven manufacturing through advanced reporting and analytics. Inspection data can be collected, monitored, and analysed to identify trends, improve processes, and reduce operational costs. METTLER TOLEDO’s ProdX software enhances this capability by centralising inspection data from multiple production lines into a single platform, providing real-time visibility and supporting paperless compliance management.
When food safety and quality are non-negotiable, METTLER TOLEDO’s Product Inspection Solutions provide the confidence manufacturers need. To see how these technologies can improve safety, quality, and efficiency within your operation, book a free personalised demonstration and experience the benefits firsthand.
Flexibility and Safety: Inspection in the Dairy Industry
By adopting this next generation of X-ray inspection, food processing plants not only safeguard...
What Makes an Enclosure Suitable for Hygienic Production?
When electrical infrastructure is installed within hygiene-critical production areas, stainless...
Beyond Ingredients: Building a Safer Food and Beverage Plant Through Better Air Quality Decisions
The future of food and beverage manufacturing depends on better decisions about everything that...