Whether it’s milk, juices or pharmaceutical products, a homogeniser is needed wherever liquids with a particularly fine texture have to be processed in order to create shelf-stable products.
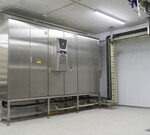
The HLI 132 from HST is a high-performance homogeniser designed for industrial applications in the food, chemical and pharmaceutical sectors, with a throughput of up to 26,500 L/h (depending on the operating pressure).
Suitable for large volume applications, the unit combines energy efficiency and sustainability through integrated valve control, internal lubrication and a compact design that eliminates the need for external cooling systems.
In the homogenising zone, particles or fat droplets are reduced in size. Thanks to a compact drive (55–132 kW) and internal lubrication, the unit does not need any additional cooling water or any external devices.
Compliant with the highest hygiene standards, it also offers aseptic options and quiet operation, making it suitable for sensitive products and modern production environments.
Phone: 0011 66 2 763 6500
EXAIR EFC Electronic Flow Control for compressed air
EXAIR's EFC Electronic Flow Control has been redesigned to make it easier to minimise...
Protect-Air CartReg inline regulator for compressed air pressure
Protect-Air's CartReg inline regulator offers a simple solution for controlling compressed...
Epicor Prism portfolio of vertical AI agents
Epicor Prism is a portfolio of vertical AI agents designed specifically for the supply chain...